



How does molecular weight affect polymer melt viscosity?




In polymer science, molecular weight is a critical factor in determining melt viscosity and processing performance. As molecular weight increases, longer polymer chains become more entangled, generally making the melt more resistant to flow. Understanding this relationship helps when comparing resin grades, interpreting rheological data, and assessing suitability for extrusion or injection molding. Molecular weight distribution, temperature, and shear rate can change the picture substantially, however, so a single flow number rarely tells the whole story.
Why longer chains make a melt harder to move
A polymer melt flows when its chains rearrange and move past one another. Short chains can generally do this more easily. As chain length increases, chains interact over a greater distance and become entangled, restricting their motion. The result is a higher resistance to flow, particularly at low shear rates where the material has time to respond as a network of interpenetrating chains.
For many linear, sufficiently entangled polymer melts, zero-shear viscosity is often approximated as proportional to the weight-average molecular weight, Mw, raised to a power of roughly 3.4. This is a useful scaling relationship, not a universal specification. It applies under defined conditions to comparable polymer chemistry and architecture; branching, temperature, additives, and differences in distribution can alter the observed behavior.
Below the entanglement region, viscosity generally grows less steeply with molecular weight. That distinction matters when comparing low-molecular-weight oligomers with commercial molding or extrusion resins: a relationship measured in one molecular-weight range should not automatically be extrapolated into another.
Average molecular weight is only part of the comparison
Commercial resins contain chains of different lengths. Number-average molecular weight, Mn, and weight-average molecular weight, Mw, describe that population differently. Mw gives greater emphasis to heavier chains, which can have a pronounced influence on melt behavior. The ratio Mw/Mn, often called dispersity, offers a broad indication of distribution width, but it does not describe the distribution’s full shape.
Two grades with similar Mw can therefore behave differently. A broader distribution may contain shorter chains that contribute to flow as well as a long-chain fraction that affects elasticity and low-shear viscosity. Long-chain branching can also increase melt elasticity and change shear response. Neither effect should be inferred from dispersity alone.
This distinction becomes practical when a processor substitutes one polyethylene grade for another. Similar melt flow rates may suggest comparable behavior under one test condition, yet the grades can respond differently in a die or during cooling. Before approving a substitution, check the resin family, density, branching, additives, and the processing data—not just the molecular-weight average or a single index.
The viscosity seen in production depends on shear
Most polymer melts are shear-thinning: their apparent viscosity decreases as shear rate increases. At low shear, a material may approach a constant zero-shear viscosity. At higher shear, chain orientation and changes in the entanglement response reduce apparent viscosity. The transition and slope depend on the material and its molecular structure.
For injection molding, resistance during rapid cavity filling can differ markedly from what a low-shear measurement suggests. In extrusion, the melt also encounters different shear conditions in the screw, the die, and after exiting the die. A grade that appears manageable at one point in the process may still cause excessive pressure, unstable output, or dimensional variation elsewhere.
A viscosity-versus-shear-rate curve at the relevant melt temperature is usually more useful than a single value. Where melt strength, die swell, or sagging is a concern, consider elastic and extensional behavior as well. Shear viscosity alone cannot establish whether an extrudate will hold its shape.
Temperature can improve flow, but it is not a free adjustment
Raising melt temperature generally lowers viscosity because chains gain mobility. That can reduce filling pressure or make extrusion easier, but more heat may also increase degradation, discoloration, or residence-time sensitivity. The acceptable window depends on the polymer, stabilizer package, equipment, and time at temperature.
If a high-molecular-weight resin needs an unusually high temperature to run, check whether the resulting process remains stable over normal production residence times. For moisture-sensitive polymers, drying is another critical control: moisture-related degradation can reduce molecular weight during processing, so the melt reaching the tool may not have the same properties as the incoming resin.
How to read melt flow rate without overreading it
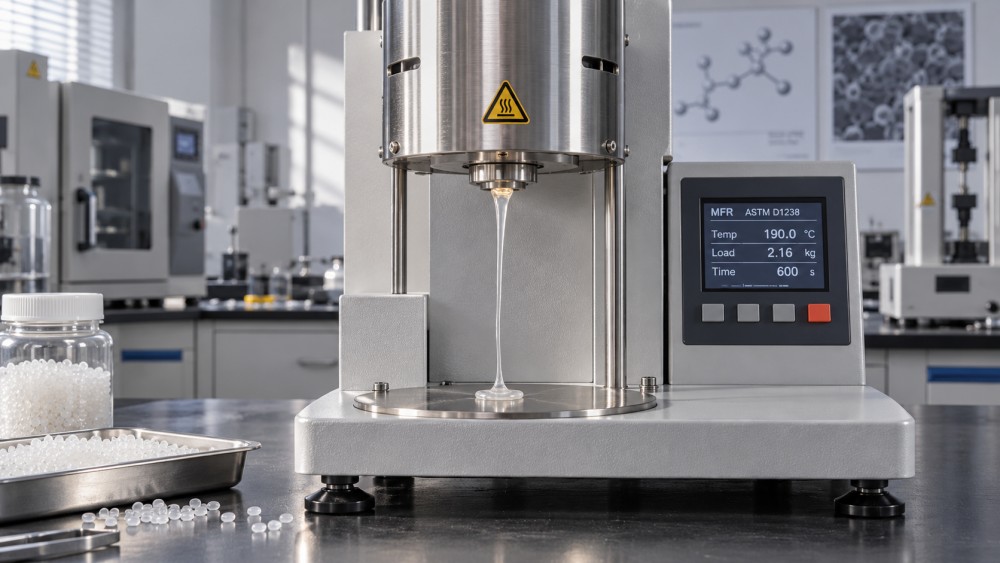
Melt flow rate (MFR), also called melt flow index, measures the mass of polymer extruded through a specified die under stated temperature and load conditions. For otherwise comparable grades tested under identical conditions, a higher MFR generally indicates lower viscosity under that test and often lower molecular weight. It is a screening tool, not a direct measurement of molecular weight or a complete rheological profile.
ASTM D1238 and ISO 1133-1 cover melt mass-flow-rate testing for thermoplastics. The reported temperature, load, conditioning, and test procedure matter; values obtained under different conditions should not be compared as though they were interchangeable. Check the current applicable standard and the material specification before using a result for acceptance.
For a closer comparison, request the following alongside MFR:
- The viscosity curve, including test temperature and shear-rate range.
- Molecular-weight distribution data, where available, with the analytical method and calibration basis identified.
- Information on branching, fillers, recycled content, and other formulation differences that may affect flow.
- Drying and processing recommendations, plus any relevant degradation limits.
Gel permeation chromatography, also known as size-exclusion chromatography, can help characterize molecular-weight distribution, but results depend on the method and calibration. Comparing numbers from different laboratories without checking those details can create false confidence.
Choosing between flow and final properties
Higher molecular weight can support properties such as toughness and resistance to slow crack growth in some polymer systems, but the benefit is material- and application-specific. It also comes with a processing trade-off: more pressure, more torque, or a narrower operating window may be needed. Lower molecular weight may ease filling or increase output, but it can leave less margin for demanding mechanical performance.
Recycled material adds another layer of uncertainty. Prior thermal and mechanical history can change molecular weight and distribution, while contamination or formulation variation can affect flow independently. A batch MFR is useful for screening, but a qualification decision may also need rheology, mechanical testing, and checks for the intended application.
When reviewing grades or supplier information through industry resources such as GEMM, use the published figures to identify candidates, then obtain comparable test conditions and current technical documents. The strongest selection is not necessarily the resin with the highest molecular weight or the easiest flow; it is the one that meets the part’s requirements within a process window the equipment can hold consistently.
- Last One:No more articles
- Next Article:How to track ore flows from the mine to the processing plantOct 30, 2026
Related News
- 00
0000-00
How does molecular weight affect polymer melt viscosity? - 00
0000-00
How to track ore flows from the mine to the processing plant - 00
0000-00
Are sodium-ion batteries suitable for cold-climate energy storage? - 00
0000-00
How to use an application compatibility guide before an OS upgrade - 00
0000-00
How overcapacity shapes the ferrous metallurgy market outlook
Related tags
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.