How to assess contamination risk in plastic recycling pellets




How to Assess Contamination Risk in Plastic Recycling Pellets
Assessing contamination risk in plastic recycling pellets is a core quality-control task because seemingly minor impurities can cause processing failures, safety concerns, rejected batches, and customer complaints.
For quality and safety teams, the objective is not simply to identify visible defects. It is to determine whether contaminants can affect performance, regulatory compliance, worker safety, or end-use reliability.
Plastic recycling pellets may contain foreign polymers, metal fragments, moisture, paper residues, residual chemicals, degraded material, black specks, fillers, or contamination from previous processing campaigns.
A practical assessment combines incoming inspection, laboratory testing, supplier documentation, process knowledge, and risk-based sampling. No single test can confirm every contamination risk in recycled polymer materials.
Quality professionals should first define the intended application. Risk tolerance differs significantly between pellets used for garden furniture, industrial packaging, automotive components, food-contact items, and electrical housings.
Higher-risk applications require stricter controls because contamination may affect migration performance, flame resistance, mechanical strength, odor, appearance, or traceability across the recycled plastics supply chain.
Start with a Risk-Based Incoming Inspection
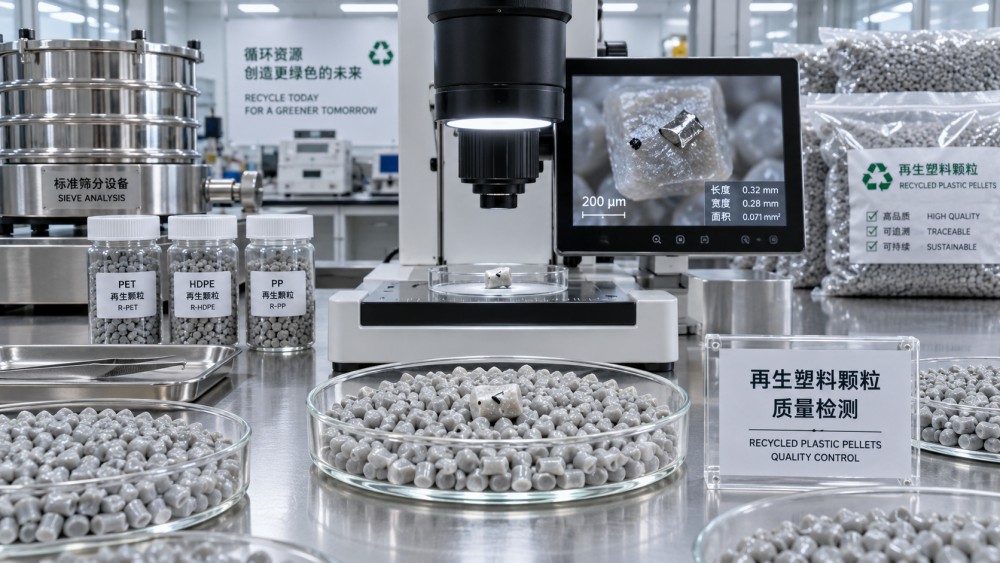
Incoming inspection should begin before pellets enter production. Review the shipment condition, packaging integrity, labeling accuracy, batch identification, color consistency, and the presence of visible foreign materials.
Collect representative samples from multiple bags, big bags, or points within a bulk delivery. Sampling only from the top layer can miss moisture pockets, segregated fines, and concentrated contaminants.
Establish a documented sampling plan based on batch size, supplier history, material type, and final application. New suppliers and high-risk applications should receive more intensive verification.
Visual inspection remains valuable because it can quickly identify black specks, colored contamination, paper fibers, wood particles, metal fragments, excessive dust, and inconsistent pellet geometry.
Record defects using a consistent acceptance system, such as particles per kilogram, percentage of off-color pellets, or photographs against a defined visual reference standard.
Pellet size variation can also indicate process instability or contamination. Excessive fines may originate from brittle degraded polymer, poor handling, screen failures, or mechanical damage during transport.
Inspect for unusual odor when opening samples. Strong chemical, burnt, solvent-like, biological, or oil odors may indicate residual contaminants requiring further laboratory investigation before use.
Identify the Contaminants That Matter Most
Incompatible polymers are among the most common and damaging contaminants in plastic recycling pellets. Even small amounts can reduce impact strength, create surface defects, and disrupt melt behavior.
For example, polyvinyl chloride contamination in recycled polyethylene or polypropylene can release corrosive compounds during processing and create discoloration, odor, and equipment maintenance problems.
Polyamide, polyethylene terephthalate, polystyrene, and multilayer packaging residues may form gels, unmelted particles, or weak interfaces when introduced into an incompatible polymer stream.
Metal contamination presents both product-quality and safety risks. Ferrous metals can damage screws and molds, while aluminum, copper, and stainless particles may escape basic magnetic separation.
Moisture is another critical risk, particularly in hygroscopic materials such as recycled PET, polyamide, polycarbonate, and certain engineering plastics. Hydrolysis can reduce molecular weight during processing.
Residual chemicals may include inks, adhesives, oils, pesticides, cleaning agents, flame retardants, or substances from the previous product use. Their relevance depends on feedstock origin and application.
Black specks require careful interpretation. They may result from carbonized polymer, degraded residues, charred contaminants, poorly cleaned equipment, or intentional black masterbatch particles in dark compounds.
Do not classify every black speck as identical. Examine frequency, particle size, hardness, distribution, and behavior during molding to distinguish normal formulation effects from process contamination.
Use Testing Methods That Match the Risk
Melt flow rate testing is a useful first indicator of recycled pellet consistency. Significant variation between batches may indicate mixed polymers, degradation, moisture exposure, or inconsistent formulation.
However, melt flow rate alone cannot identify the contaminant. Use it alongside visual inspection, density testing, ash content, moisture analysis, and processing trials for a more reliable decision.
Fourier-transform infrared spectroscopy, commonly called FTIR, can help identify unknown polymer fragments and confirm whether a suspect particle differs from the declared base resin.
Differential scanning calorimetry can identify melting transitions associated with incompatible polymers. It is particularly useful when recycled pellets may contain polypropylene, polyethylene, PET, or polyamide mixtures.
Thermogravimetric analysis can support evaluation of filler content, volatile residues, and thermal stability. Unexpected ash levels may suggest excess mineral filler, dirt, pigments, or inorganic contamination.
Moisture analyzers should be used before processing, especially when pellets are stored in humid environments. Measure both average moisture and variability between sampled packages when practical.
Metal detectors and magnets provide effective production-line controls, but their limits must be understood. Nonferrous metal detection and fine particle detection may require specialized equipment settings.
For sensitive applications, consider gas chromatography, mass spectrometry, or targeted migration testing. These methods are appropriate when odor, residual chemicals, or regulatory substances create material-use concerns.
Evaluate Suppliers Beyond the Certificate of Analysis
A certificate of analysis is useful, but it should not replace supplier qualification. Review whether reported values reflect every batch, periodic testing, or only a general product specification.
Ask suppliers to describe feedstock sources, sorting technologies, washing steps, melt filtration, degassing systems, metal separation, and quality checks used before pelletizing.
Feedstock traceability is especially important for plastic recycling pellets intended for regulated sectors. Post-industrial streams are generally easier to control than mixed post-consumer waste streams.
Supplier risk increases when the feedstock includes unknown imported scrap, mixed municipal waste, heavily printed packaging, agricultural films, electronic waste, or materials with unclear previous use.
Review batch traceability procedures, complaint handling, retained sample practices, change-control processes, and methods used to prevent cross-contamination between different polymer grades and colors.
Site audits can reveal controls that documents do not show. Observe storage conditions, housekeeping, screening equipment, material identification, regrind handling, and segregation between production lines.
Request trend data rather than isolated test results. A supplier with stable monthly results and transparent corrective actions may present lower risk than one providing only compliant individual certificates.
Confirm Risk Through Processing Trials
A controlled processing trial is often the most practical way to evaluate whether contamination will affect the intended manufacturing process. Use representative equipment and normal operating conditions.
Monitor melt pressure, torque, screen-pack loading, venting behavior, color changes, odor, die buildup, surface finish, and the frequency of gels or unmelted particles.
Unexpected pressure increases may indicate contamination, poor filtration, excessive fines, or polymer incompatibility. Record baseline conditions for approved materials to identify meaningful deviations quickly.
For injection molding, assess flow marks, splay, short shots, weld-line strength, black specks, and part appearance. For extrusion, inspect film consistency, gels, thickness variation, and die deposits.
Test finished properties relevant to the application, including tensile strength, impact resistance, elongation, density, hardness, and dimensional stability. Compare results with approved virgin or recycled benchmarks.
When a batch performs acceptably in a short trial, do not assume unlimited approval. Confirm that the batch remains stable during full production runs and repeat processing cycles.
Set Clear Acceptance Limits and Escalation Rules
Quality decisions become more consistent when acceptance limits are written before deliveries arrive. Define limits for moisture, metal detection, melt flow variation, ash content, visual defects, and odor.
Limits should reflect the final product, not only the pellet specification. A cosmetic consumer product may prioritize color and specks, while a structural part may prioritize mechanical consistency.
Create escalation rules for borderline material. For example, a batch may be quarantined, downgraded to a lower-risk application, blended under controlled conditions, returned, or sent for additional testing.
Quarantine procedures should prevent accidental release into production. Physically segregate suspect pellets, update inventory status, retain samples, and document the reason for investigation and final disposition.
Corrective actions should address root causes rather than only reject individual loads. Repeated contamination may require supplier audits, tighter specifications, revised sampling frequency, or alternative sourcing.
Track complaints, production interruptions, test failures, and visual defect rates by supplier and batch. Trend analysis helps reveal chronic risks that isolated inspection results may not expose.
Build a Practical Contamination-Control System
An effective contamination-control system begins with material classification. Separate approved grades by polymer type, color, source, application risk, and known limitations before storage or production use.
Use dedicated storage areas, clearly labeled containers, clean transfer equipment, and documented line-clearance procedures. Internal cross-contamination can undermine even well-qualified recycled material suppliers.
Maintain retained samples from each accepted batch. These samples support complaint investigations, comparison testing, supplier discussions, and verification when defects appear after downstream processing.
Train operators to recognize early warning signs, including unusual odor, screen changes, increased pressure, inconsistent color, excessive dust, or unexpected changes in molded-part appearance.
For high-risk products, combine supplier approval with routine verification testing. This layered approach is more dependable than relying on visual checks, paperwork, or a single laboratory result.
Conclusion
Contamination risk in plastic recycling pellets should be assessed as a material-performance and product-safety issue, not merely as a visual-quality concern.
The strongest decisions combine representative sampling, targeted testing, supplier process evaluation, controlled processing trials, and clear acceptance limits tied to the intended application.
By treating recycled pellets as a managed technical material rather than an interchangeable commodity, quality and safety teams can reduce disruptions, protect product performance, and improve sourcing confidence.
Related News
- 00
0000-00
How to assess contamination risk in plastic recycling pellets - 00
0000-00
Can biofuels for industrial boilers reduce fuel costs at high load? - 00
0000-00
How to assess the reliability of offshore drilling safety systems - 00
0000-00
How to verify quality systems at oil and gas industry suppliers - 00
0000-00
Which carbon capture materials grades suit high-humidity flue gas?
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.